Advantages of Anti-fog BOPP Film in Medical Packaging

Summary
Anti-fog BOPP (biaxially oriented polypropylene) film is revolutionizing medical packaging by addressing critical challenges in sterility, visibility, and safety. This innovative material offers exceptional clarity and condensation resistance, ensuring that packaged contents remain visible and uncontaminated. Its durable and moisture-resistant properties make it ideal for maintaining the integrity of sterile environments, while its compliance with global regulatory standards such as FDA guidelines and ISO 11607 ensures reliability and trustworthiness in healthcare settings. The film is widely used for packaging sterile medical devices like scalpels and syringes, pharmaceutical products including liquid medications and ampoules, wound dressings, bandages, surgical kits, and pre-packaged medical supplies. By enhancing visibility, anti-fog BOPP film enables quick identification of contents, reducing the risk of contamination and human error. It also improves compliance with safety standards, contributing to a reduction in hospital-acquired infections (HAIs).
What is Anti-fog BOPP Film?
To truly understand the benefits of anti-fog BOPP film in medical packaging, it’s important to first understand what it is and how it works. BOPP stands for biaxially-oriented polypropylene, which is a type of film created by stretching polypropylene (PP) in two directions—both lengthwise and widthwise. This unique orientation improves the material’s strength, clarity, and resistance to moisture, making it ideal for packaging applications in various industries.
The anti-fog aspect comes from a special coating or treatment applied to the surface of the film. This treatment prevents condensation from forming on the surface of the film, which can obscure the visibility of the product inside. By minimizing fog buildup, the film maintains its clarity, ensuring that medical products are visible at all times, whether on a shelf, in transit, or during patient use.
This anti-fog technology is particularly crucial in environments like healthcare facilities, where visibility, cleanliness, and sterility are top priorities. Whether packaging sterile medical devices or pharmaceuticals, the anti-fog BOPP film ensures that medical products are not only well-protected but also easily identifiable when needed.

Key Properties of Anti-fog BOPP Film
The anti-fog BOPP film comes with a unique set of properties that distinguish it from traditional medical packaging materials. These key features contribute to its growing importance in the medical packaging industry.
1. Exceptional Clarity and Transparency
One of the primary benefits of anti-fog BOPP film is its exceptional clarity. The film is highly transparent, offering excellent visibility of the contents inside. For medical packaging, this is incredibly important. Healthcare professionals need to quickly identify products without compromising sterility or safety. The clarity provided by anti-fog BOPP films allows for quick inspection of medical items such as syringes, bandages, and wound dressings, making it easier to verify the contents and expiration dates without unnecessary handling or opening of packages.
2. High Barrier Protection
Another key advantage of anti-fog BOPP film is its high barrier protection against moisture, oxygen, and contaminants. For medical packaging, maintaining the integrity of the contents is vital. BOPP films inherently offer strong protection against moisture, which is essential in preventing microbial growth and contamination. This barrier capability makes anti-fog BOPP films ideal for packaging pharmaceuticals such as liquid medications, ampoules, and diagnostic kits, ensuring that the active ingredients remain stable and effective until they are used.
3. Resistance to Tears and Punctures
BOPP films, including the anti-fog version, exhibit remarkable mechanical properties that make them resistant to tears and punctures. This feature is crucial for maintaining the sterility of medical products during shipping, storage, and handling. Medical devices, particularly those used in sterile environments, must remain intact and protected until they are ready for use. Anti-fog BOPP films ensure that even with rough handling or transport, the packaging remains intact, and the contents are protected from external contamination.
4. Reduced Risk of Condensation Buildup
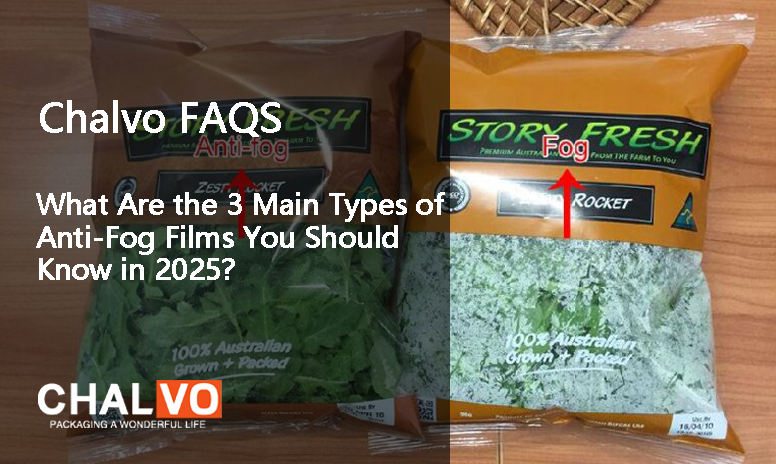
One of the most significant challenges in medical packaging is condensation, particularly in humid or temperature-fluctuating environments like healthcare facilities or during transportation. Traditional packaging films often trap moisture inside, leading to fog or condensation on the surface. This can obscure the visibility of the product and, more importantly, can lead to microbial contamination. However, anti-fog BOPP film is specifically designed to prevent condensation from forming on the film’s surface. By eliminating this issue, the film helps maintain clarity and cleanliness, ensuring that medical products are visible and free from contamination.
Key Properties of Anti-fog BOPP Film
The anti-fog BOPP film comes with a unique set of properties that distinguish it from traditional medical packaging materials. These key features contribute to its growing importance in the medical packaging industry.
1. Exceptional Clarity and Transparency
One of the primary benefits of anti-fog BOPP film is its exceptional clarity. The film is highly transparent, offering excellent visibility of the contents inside. For medical packaging, this is incredibly important. Healthcare professionals need to quickly identify products without compromising sterility or safety. The clarity provided by anti-fog BOPP films allows for quick inspection of medical items such as syringes, bandages, and wound dressings, making it easier to verify the contents and expiration dates without unnecessary handling or opening of packages.
2. High Barrier Protection
Another key advantage of anti-fog BOPP film is its high barrier protection against moisture, oxygen, and contaminants. For medical packaging, maintaining the integrity of the contents is vital. BOPP films inherently offer strong protection against moisture, which is essential in preventing microbial growth and contamination. This barrier capability makes anti-fog BOPP films ideal for packaging pharmaceuticals such as liquid medications, ampoules, and diagnostic kits, ensuring that the active ingredients remain stable and effective until they are used.
3. Resistance to Tears and Punctures
BOPP films, including the anti-fog version, exhibit remarkable mechanical properties that make them resistant to tears and punctures. This feature is crucial for maintaining the sterility of medical products during shipping, storage, and handling. Medical devices, particularly those used in sterile environments, must remain intact and protected until they are ready for use. Anti-fog BOPP films ensure that even with rough handling or transport, the packaging remains intact, and the contents are protected from external contamination.
4. Reduced Risk of Condensation Buildup
One of the most significant challenges in medical packaging is condensation, particularly in humid or temperature-fluctuating environments like healthcare facilities or during transportation. Traditional packaging films often trap moisture inside, leading to fog or condensation on the surface. This can obscure the visibility of the product and, more importantly, can lead to microbial contamination. However, anti-fog BOPP film is specifically designed to prevent condensation from forming on the film’s surface. By eliminating this issue, the film helps maintain clarity and cleanliness, ensuring that medical products are visible and free from contamination.
Applications of Anti-fog BOPP Film in Medical Packaging
The applications of anti-fog BOPP film in medical packaging are vast, encompassing everything from sterile medical devices to pharmaceuticals. Below are some of the key areas where this innovative material plays a critical role:
1. Sterile Medical Devices
Anti-fog BOPP film is widely used in the packaging of sterile medical devices, such as scalpels, syringes, and surgical tools. In medical settings, where sterility is paramount, it is essential that the packaging maintains clarity so that the contents can be inspected without breaking the seal. The anti-fog coating ensures that the contents remain visible even in humid or refrigerated environments. This is crucial for ensuring that medical professionals can quickly and easily check the contents without the need for unnecessary handling or unsealing, which could compromise sterility.
2. Pharmaceuticals and Medical Consumables
Another major application of anti-fog BOPP film is in the packaging of liquid pharmaceuticals, ampoules, and other medical consumables. These products often require high levels of protection to maintain their efficacy and prevent contamination. The high barrier properties of BOPP films prevent the ingress of moisture and oxygen, which could degrade the quality of the pharmaceutical product. The anti-fog feature ensures that the packaging remains clear, even if the product is exposed to varying temperature and humidity conditions during transit and storage.
3. Wound Dressings and Bandages
In addition to medical devices and pharmaceuticals, anti-fog BOPP film is also used to package wound dressings and bandages. These products must remain sterile and protected from external contaminants while ensuring that their sterility can be verified quickly and easily. The anti-fog properties of the BOPP film make it easier for healthcare workers to inspect the products without compromising the packaging’s integrity or cleanliness.
4. Surgical Kits and Pre-packaged Products
Surgical kits, which contain pre-sterilized instruments and supplies for use in operating rooms, also benefit from anti-fog BOPP film packaging. The clarity and condensation resistance of the film allow surgical staff to quickly verify the contents of the kits without needing to open them. This saves valuable time in high-pressure environments like operating rooms, where every second counts. By ensuring that the contents of the kits are visible and intact, anti-fog BOPP film enhances the overall efficiency and safety of medical procedures.
Benefits for Healthcare Professionals and Hospitals
The use of anti-fog BOPP film not only benefits the products being packaged but also has a positive impact on healthcare professionals and hospital settings.
1. Enhanced Visibility for Rapid Decision-Making
In emergency rooms and operating rooms, healthcare professionals need to make quick decisions. Anti-fog BOPP film allows medical staff to easily identify products without removing them from their packaging or exposing them to contaminants. This is especially crucial in situations where time is critical, as the ability to rapidly assess the contents of sterile packs and kits can have a direct impact on patient outcomes.
2. Minimizing Handling Risks
By maintaining the integrity of the packaging and eliminating the need for unnecessary handling, anti-fog BOPP film reduces the risk of contamination and human error. This minimizes the chances of packaging failure, contamination, and mishandling, all of which are potential sources of hospital-acquired infections (HAIs). This leads to better patient safety and improved overall hospital hygiene.
3. Compliance with Global Standards
In an increasingly regulated industry, ensuring compliance with global packaging standards is critical. Anti-fog BOPP film packaging meets FDA guidelines and ISO 11607, which are international standards for sterile medical packaging. This compliance guarantees that the packaging adheres to the highest quality standards, ensuring that the products inside are safe and effective for use.
The Future of Anti-fog BOPP Film in Medical Packaging
Looking ahead, the future of anti-fog BOPP film in medical packaging looks incredibly promising. Advancements in materials science and nanotechnology are likely to result in even more sustainable and efficient solutions. For instance, the integration of biodegradable coatings may provide a more eco-friendly alternative to traditional packaging, aligning with the growing trend toward sustainability in healthcare. Additionally, the incorporation of RFID tags and temperature-sensitive indicators could further enhance the functionality of anti-fog BOPP films, enabling real-time tracking and ensuring the quality and safety of pharmaceuticals during transportation.
Contact us
At Chalvo, we understand the unique needs of businesses looking to enhance their packaging, marketing materials.
Our team is here to help you choose the right laminating films that not only meet your functional needs but also help elevate your brand’s visual appeal.