What is heat-sealable film?

Summary
In the packaging industry, heat-sealable films play a crucial role in ensuring the secure and efficient sealing of products. These films are essential in a wide range of applications, from food packaging to industrial wraps. This article explores what heat-sealable films are, the materials used to create them, and the concept of heat sealability. By understanding these aspects, packaging professionals and manufacturers can better select the right film for their needs.
Highlights
- Heat Sensitivity: These films respond to specific temperature ranges, allowing them to bond securely.
- Durability: They offer a reliable seal that protects the product from contaminants, moisture, and air exposure.
- Versatility: Heat-sealable films are available in various thicknesses and finishes, making them suitable for different packaging applications.
What Materials Are Heat-Sealable?
Several materials are used in the production of heat-sealable films, each offering unique properties based on the intended application. Here are some common heat-sealable materials:
Polyethylene (PE)
Polyethylene is one of the most widely used heat-sealable materials. It is known for its flexibility, moisture resistance, and durability. PE is used in a variety of applications, including food packaging, agricultural films, and consumer products. There are different types of polyethylene films, such as LDPE (Low-Density Polyethylene) and HDPE (High-Density Polyethylene), each offering varying levels of strength and sealability.
Polypropylene (PP)
Polypropylene is another popular heat-sealable material known for its clarity, strength, and chemical resistance. BOPP (Biaxially Oriented Polypropylene) and CPP (Cast Polypropylene) are commonly used in applications that require strong seals and visual appeal, such as snack packaging and food wraps.
Polyester (PET)
Polyester films provide excellent clarity, strength, and barrier properties. They are often coated with heat-sealable layers, making them ideal for applications that require both visual clarity and strong seals, such as vacuum packaging and medical packaging.
PVC (Polyvinyl Chloride)
PVC films are known for their flexibility and durability. Although not as commonly used today due to environmental concerns, PVC remains an option for certain applications requiring a secure seal and specific chemical resistance properties.
Polyolefin Shrink Films
Polyolefin films are used in applications that require a tight, shrinkable wrap around a product. These films offer strong sealability and durability, making them ideal for retail packaging and protective wraps.
What is the Meaning of Heat Sealability?
Heat sealability refers to the ability of a material or film to form a bond when heat and pressure are applied. This property is critical in packaging applications where creating a secure, airtight seal is essential for maintaining product integrity and freshness.
Factors Affecting Heat Sealability:
- Seal Temperature: The specific temperature at which a film begins to bond effectively.
- Pressure: The amount of pressure applied during the sealing process can affect the strength and quality of the seal.
- Dwell Time: The amount of time that heat and pressure are applied to the film to create a bond.
- Coatings and Additives: Many heat-sealable films are treated with coatings or additives that enhance their sealability, allowing them to bond at lower temperatures or provide stronger seals.
Heat sealability is a vital property in the packaging industry because it ensures that products remain securely sealed, preventing contamination, spoilage, or tampering.
Applications of Heat-Sealable Films in Packaging
Heat-sealable films are used across various industries due to their versatility and reliability. Some common applications include:
Food Packaging
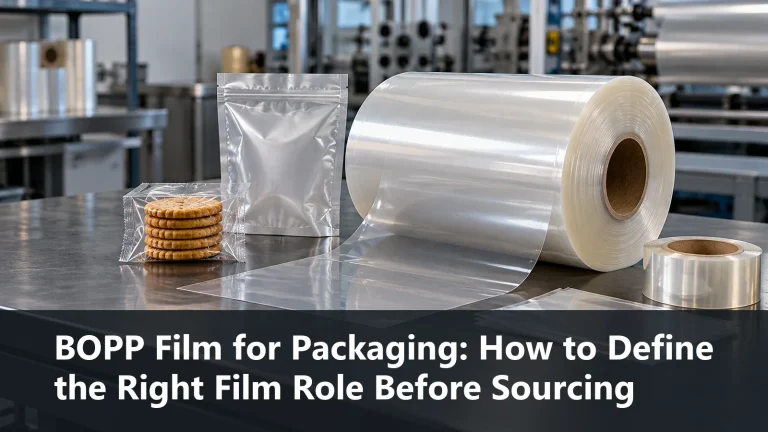
Heat-sealable films are extensively used in food packaging to create secure, airtight seals that protect products from moisture and contaminants. These films are found in snack bags, frozen food packaging, and vacuum-sealed products.
Pharmaceutical Packaging
In the pharmaceutical industry, maintaining product integrity and safety is crucial. Heat-sealable films provide tamper-evident packaging solutions for medicines, ensuring that they are protected from external elements.
Industrial and Protective Packaging
Heat-sealable films are used in industrial applications to wrap and protect products during transportation and storage. These films provide a secure seal, preventing damage or contamination of goods.
Consumer Goods and Retail Packaging
In consumer goods, heat-sealable films are commonly used for retail packaging to enhance the shelf appeal of products while providing a strong, protective barrier. Products like toys, electronics, and cosmetics often use heat-sealable films for secure and attractive packaging.
Choosing the Right Heat-Sealable Film
Selecting the right heat-sealable film depends on several factors, including the type of product being packaged, the desired barrier properties, and the sealing equipment being used. Here are some tips for choosing the right film:
- Consider the Application: Determine the specific requirements of the product, such as moisture resistance, clarity, or tamper evidence.
- Evaluate the Material: Choose a material that offers the necessary seal strength and flexibility for your application. For example, PE is ideal for moisture resistance, while BOPP is suitable for high-clarity applications.
- Check Compatibility with Sealing Equipment: Ensure that the film is compatible with your sealing equipment, considering factors like temperature and pressure requirements.
- Look for Customization Options: Many manufacturers offer custom films with tailored properties, such as special coatings or additives that enhance seal strength or barrier performance.
Partnering with a Reliable Flexible Films Manufacturer in China
For packaging professionals and manufacturers looking to source high-quality heat-sealable films, partnering with a reliable flexible films manufacturer in China offers several advantages:
- Large Production Capacity: Manufacturers in China can meet large-scale demands, providing consistent quality at competitive prices.
- Customization Options: Many manufacturers offer customization options to meet the unique needs of their clients, such as specific thicknesses, coatings, and finishes.
- Certified Quality: Chinese manufacturers often adhere to international standards, ensuring that their products meet safety and quality regulations.