



A printable BOPP roll can look correct at receipt and still cause weak adhesion, rub, curl, delamination, or sealing issues after conversion. The cause may sit at the treated surface, ink, adhesive, cure, winding, tension, or finished-pack stage.
Printable BOPP may be considered as an outer or print web in flexible packaging, but printability is a grade- and process-specific property. Buyers should confirm the treated side, ink and adhesive system, conversion sequence, and finished-laminate test plan before approving a roll.
Use these questions to make the inquiry usable for a converter and supplier.

What does “printable BOPP” mean?
Printable BOPP is a BOPP film selected or treated for an intended printing or conversion role. It is usually discussed as an outer web or print carrier in a laminate, not as a complete pouch specification.
Establish:
- Exact grade, nominal thickness, and treated/print side.
- Print process, ink or coating system, and cure route.
- Laminate structure, roll format, winding direction, and handling conditions.
- Final sealing, barrier, and distribution requirements.
A printing-grade web can be the right starting point for a package, while the sealant and barrier functions are carried by other layers. Do not presume that a printable BOPP grade is also heat sealable, high barrier, or suitable for direct food contact in the finished application.
Why does the treated side matter?
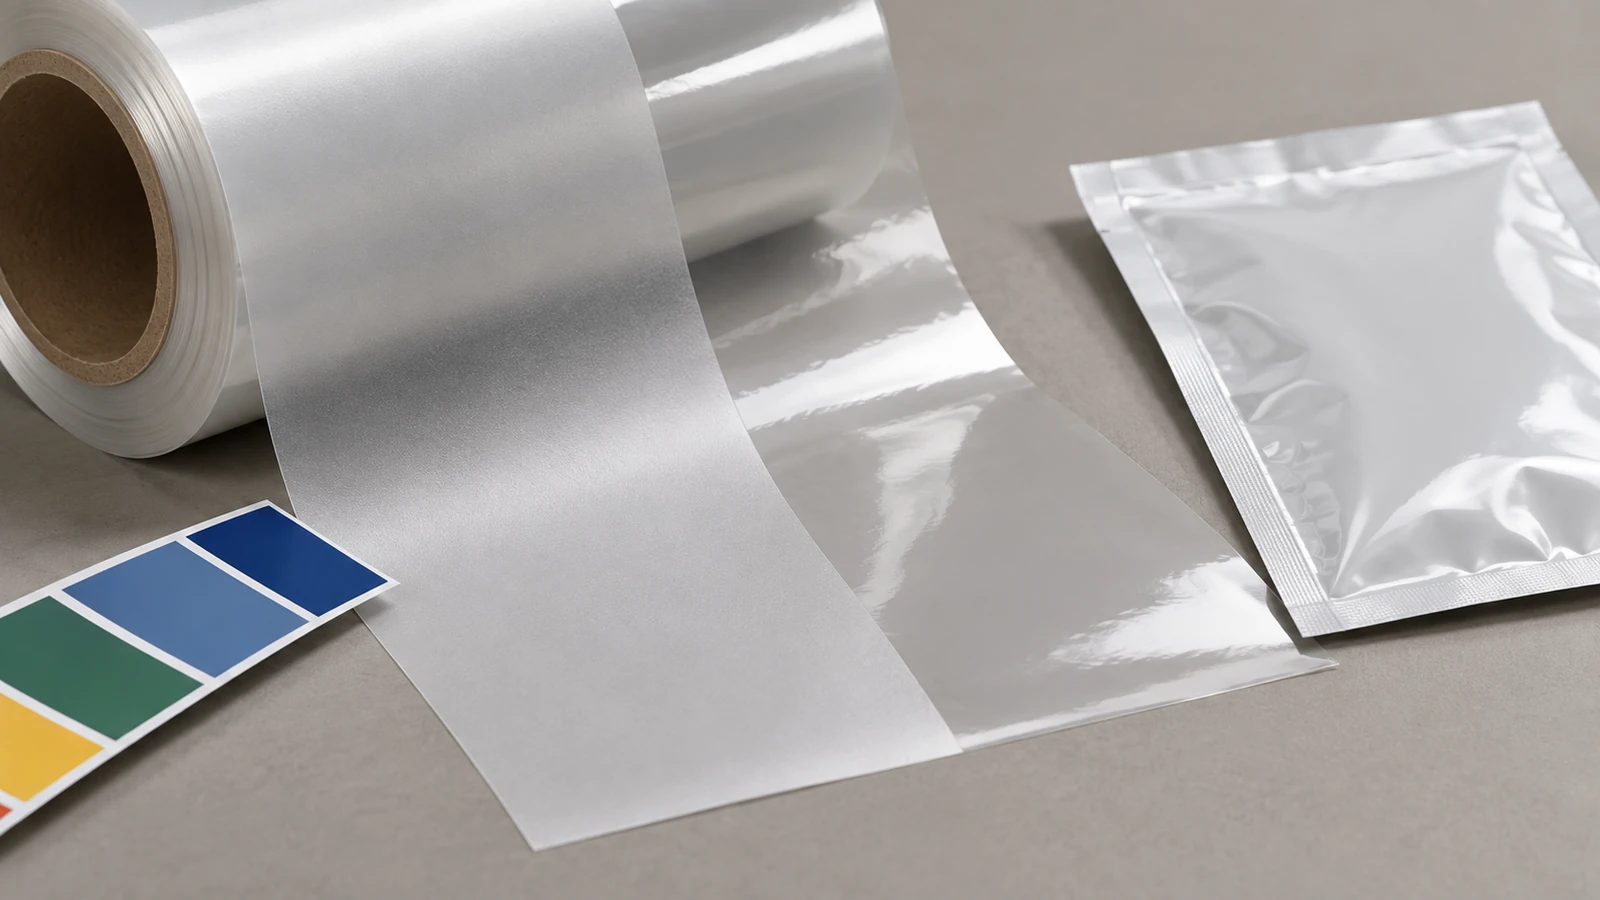
Surface treatment can help create a surface that is intended to receive ink, coating, or adhesive. It does not guarantee print adhesion in every converting system.
The buyer, printer, and supplier need the same treated-side reference. Printing the wrong side may only become apparent after cure, lamination, or a rub test.
Before a trial, record:
| Item | What to confirm |
|---|---|
| Film identity | Grade name, roll ID, nominal thickness, available production or inspection record |
| Treated surface | Which side is treated, its orientation on the roll, and how it will reach the print station |
| Ink system | Ink family, color design, primer or overprint varnish, and cure conditions |
| Lamination | Adhesive system, relevant application controls, cure schedule, and opposing web |
| Process | Tension, speed, temperature exposure, static control, and machine path |
| Test | Adhesion/rub method, observation point, sample conditioning, and acceptance criteria |
A dyne value or surface-treatment statement without the ink system, storage history, method, and acceptance rule is incomplete evidence. Treatment level can be one variable in an adhesion problem, but it is not the only one.
Can printable BOPP be used in any flexible package?
No. The final application decides whether a printable BOPP web is appropriate.
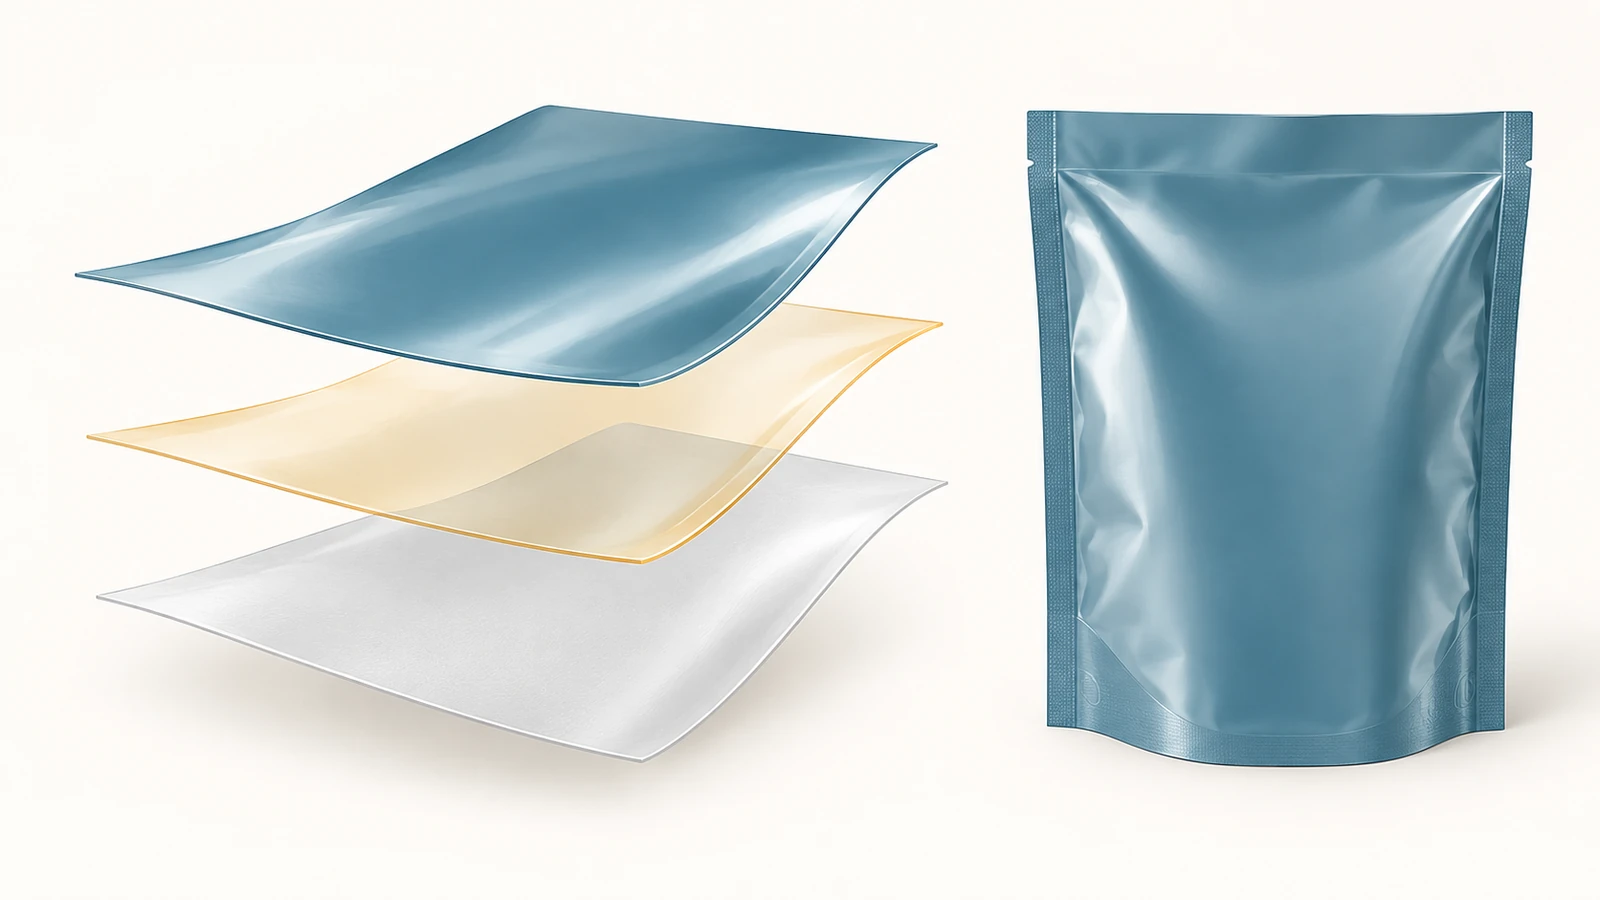
Packages may all use printed webs while having different risks and structures. The outer web may carry graphics while other layers provide sealing, mechanical support, or a defined barrier function.
Map the package before comparing films:
| Layer role | Buyer question | Evidence required |
|---|---|---|
| Printable outer BOPP | Is it suitable for the intended print and lamination route? | Grade-specific information plus printed/laminated trial observations |
| Adhesive or tie layer | Is it compatible with the two nominated substrates and planned conversion route? | Supplier process guidance and laminate-level checks |
| Functional barrier layer | Which risk is it intended to address: oxygen, water vapor, aroma, or light? | Structure-specific data with method, units, thickness, and conditions |
| Sealant layer | What surface seals, under which settings, and with what contamination conditions? | Seal-interface and finished-pack evidence |
| Finished package | Does the actual package meet its product and distribution criteria? | Application-specific validation plan and results |
This approach prevents a common error: approving a good-looking printed web before defining whether the complete package has the right sealing and protection functions.
Which print-and-lamination route should a buyer compare first?
Start with the least complex route that addresses the known package risk; complexity is not a price, performance, MOQ, or lead-time promise.
| Route complexity | Useful starting condition | What still has to be confirmed |
|---|---|---|
| Lower | A routine printed outer web in an already validated structure | Treated side, ink/cure, roll handling, and whether the prior structure is truly comparable |
| Medium | A new printed BOPP web plus a nominated adhesive and opposing web | Laminate compatibility, cure, tension balance, appearance and downstream seal behavior |
| Higher | Multiple functional layers or a demanding shelf-life, visual, or converting target | Full structure, layer responsibilities, method-specific evidence, line window and finished-pack validation |
The right route depends on the product risk and the existing process baseline. A more complex laminate does not correct an undefined print, adhesive, or cure condition.
Which BOPP document categories should a buyer request?
The CHALVO knowledge base has buyer-facing documents for printing-grade, shallow-screen printing-grade, matt printing-grade, and lamination-film categories. They are only candidate-category leads.
For the exact candidate, request the current TDS and ask:
- Does the grade, treatment, and thickness match the proposed roll and intended print or lamination side?
- Which ink, adhesive, coating, cure, test conditions, storage guidance, and trial scope apply?
A general product-family description does not support production approval.
What causes print rub, poor adhesion, or inconsistent appearance?
Several variables can contribute; record the condition before changing material.
| Observation | Possible variables | Records that make the next step useful |
|---|---|---|
| Ink rubs or lifts | Treated side, surface condition, ink selection, curing, varnish, roll age, storage | Roll ID, print sequence, ink batch, cure conditions, rub-test method, photos |
| Print looks uneven | Ink transfer, anilox/plate settings, surface variation, static, web tension, line speed | Machine settings, web direction, ambient condition, defect location and repeatability |
| Laminate curls or distorts | Tension balance, adhesive, cure, opposing web, heat history, winding | Full structure, unwind direction, tension settings, adhesive system, cure time and curl orientation |
| Delamination occurs | Adhesive selection/application, treatment, contamination, cure, substrate mismatch | Failure interface, sample history, process record, test method, storage condition |
| Pouch seal changes after printing/lamination | Sealant choice, migrated variables, structure, heat history, machine settings | Seal interface, completed structure, sealing settings, product contamination and test result |
No observation proves a root cause by itself. It supports a controlled trial rather than a generic printability claim.
Does printable BOPP determine barrier performance?
No. A printable outer web and a barrier package are different concepts.
If the package needs oxygen, water-vapor, aroma, light, or other protection, identify the responsible layer and test. A number is comparable only with method, unit, thickness, structure, temperature, and humidity condition.
Do not infer:
- Oxygen performance from a water-vapor result, or the reverse.
- A laminate result from a base-web result.
- Finished-pouch shelf life from a film description.
- Food-contact suitability from a general BOPP label.
- A barrier claim from a surface finish or print property.
For a shelf-life target, the validation plan needs the actual structure, product, storage route, seals, and destination-market documentation.
How should buyers set up a printable BOPP trial?
Use a one-variable trial wherever practical.
- Freeze the baseline: current film, grade, roll ID, print and adhesive system, structure, machine settings, speed, and failure signal.
- Change one factor, such as a nominated grade, surface orientation, or conversion setting.
- Set acceptance criteria: appearance, adhesion/rub test, laminate appearance, curl, seal behavior, and route-relevant handling check.
- Assess the finished structure, then decide with the supplier and converter which variable to test next.
This does not guarantee production performance; it makes qualification traceable.
Printable BOPP RFQ checklist
Include these details when asking for a sample or quotation:
- Product, pack format, and the printable BOPP web’s intended role.
- Proposed laminate structure, with known layer order and nominal thicknesses.
- Required appearance: gloss, matte, transparency, opacity, or other defined outcome.
- Print process, ink/coating system, and whether reverse printing is planned.
- Lamination adhesive, opposing substrate, and planned cure conditions.
- Machine type, width, speed, tension, static controls, winding direction, core, and roll format.
- Target market, required documents, sample quantity, test method, and acceptance criteria.
- Any existing failure: photos, roll IDs, print/lamination settings, and where the defect appeared.
CHALVO can help coordinate candidate-grade information, current documents, and sample scope. Final grade selection, availability, compliance documentation, conversion performance, and finished-package suitability require project confirmation.
FAQ
Is printing-grade BOPP automatically suitable for lamination?
No. The specific grade, treated side, adhesive system, cure, opposing web, tension conditions, and final package all need to be confirmed.
Can printable BOPP be heat sealed?
Do not assume so. Printing and sealing are different roles. Confirm whether the specific grade is designed to seal, the opposing surface, and the real line conditions.
What should I ask for before approving a printable BOPP sample?
Ask for the exact current grade information, intended treated/print side, relevant test conditions, storage guidance, and a trial plan that includes the printed and laminated final structure.
Does a treatment statement prove ink adhesion?
No. It can be a useful part of the candidate-grade discussion, but adhesion should be checked against the nominated ink system, coating or varnish, cure route, sample history, test method, and acceptance criteria.
Related buyer guides
- For the material definition and limits, see What Is BOPP Film? A Packaging Buyer Guide to Structure, Uses and Limits.
- For a controlled bonding-trial approach, see How to Glue Polypropylene: A Controlled Bonding Trial Guide.
- For a heat-seal selection question, see Heat-Sealable BOPP for Seasoning Sachets: What to Check Before Filling.
Summary
Printable BOPP can be a strong candidate for the right flexible-package outer web, but a film’s surface is only one part of conversion success. Specify the grade and treated side, control the ink and lamination variables, and validate the completed structure on the actual line before approval.