


Summary
In the modern food packaging industry, ensuring freshness, durability, and visual appeal is essential. BOPP heat sealable film has become a preferred choice for flexible packaging due to its superior sealing properties, high transparency, and excellent barrier protection. This specialized biaxially oriented polypropylene (BOPP) film offers enhanced product safety, extended shelf life, and improved efficiency in packaging processes.
This article explores the advantages of BOPP heat sealable film for food applications, covering its key benefits, applications, technical properties, and industry relevance.
1. What Is BOPP Heat Sealable Film?
📌 Definition & Composition
BOPP heat sealable film is a type of biaxially oriented polypropylene (BOPP) film engineered with heat-sealing properties, making it ideal for food packaging and labeling. The film can be single-side or double-side heat sealable, depending on the packaging requirements.
📌 Key Characteristics
✔ Strong heat sealing – Ensures secure packaging integrity
✔ High transparency & gloss – Enhances visual appeal for consumers
✔ Excellent moisture & contamination barrier – Maintains food freshness
✔ Lightweight & flexible – Improves packaging efficiency and reduces costs
✔ Customizable thickness & size – Suitable for various packaging designs
With these properties, BOPP heat sealable film is widely used in snacks, confectionery, frozen foods, and fresh produce packaging.
2. Why Choose BOPP Heat Sealable Film for Food Packaging?
📌 Superior Heat Sealing Performance
✔ Tight & secure sealing – Prevents leakage, contamination, and spoilage
✔ Ideal for high-speed packaging machines – Ensures efficiency & consistency
✔ Custom heat seal range (115-140°C) – Adaptable for various food applications
📌 Enhanced Product Protection
✔ Strong moisture barrier – Keeps food fresh & crispy
✔ Oxygen resistance – Reduces oxidation & extends shelf life
✔ Prevents external contamination – Ensures hygienic food storage
📌 High Clarity & Visual Appeal
✔ Crystal-clear transparency – Showcases products attractively
✔ Glossy finish – Enhances brand presentation & shelf impact
✔ Excellent printability – Supports high-quality branding & labeling
📌 Sustainability & Cost-Effectiveness
✔ Lightweight material – Reduces packaging waste & shipping costs
✔ Recyclable – Supports environmentally friendly packaging solutions
✔ Compatible with laminations – Enhances functionality without excessive materials
3. Common Applications of BOPP Heat Sealable Film in Food Packaging
BOPP heat sealable film is widely used in food packaging due to its protective and aesthetic qualities. Some of its main applications include:
📦 Snack & Confectionery Packaging
✔ Chips, nuts, and popcorn – Keeps crispness & prevents moisture absorption
✔ Candies & chocolates – Maintains flavor & prevents oxidation
📦 Frozen & Fresh Food Packaging
✔ Frozen vegetables & fruits – Protects against freezer burn & contamination
✔ Meat & seafood – Prevents leakage while ensuring hygiene
📦 Bakery & Dry Food Packaging
✔ Bread & biscuits – Maintains freshness & crisp texture
✔ Pasta & cereals – Provides long-term protection from humidity
📦 Beverage & Dairy Product Packaging
✔ Milk powder & coffee – Prevents clumping & moisture penetration
✔ Juice & yogurt lids – Ensures secure sealing & leak prevention
📦 Ready-to-Eat Meal Packaging
✔ Instant noodles & microwave meals – Heat-resistant for safe reheating
✔ Pre-packaged salads – Keeps ingredients fresh & crisp
📦 Specialty Packaging for Premium Products
✔ High-end chocolates & gourmet foods – Enhances luxury branding
✔ Organic & health food packaging – Provides eco-friendly & secure sealing
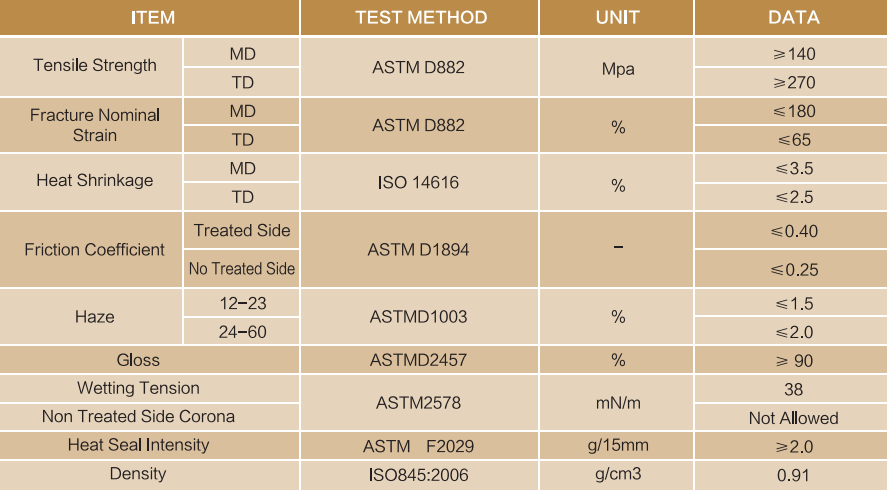
4. Technical Properties of BOPP Heat Sealable Film
These properties make BOPP heat sealable film highly reliable for food safety, durability, and efficient processing.

5. How BOPP Heat Sealable Film Enhances Food Safety & Sustainability
📌 Ensuring Food Safety & Hygiene
🔹 Non-toxic & food-grade material – Meets FDA & EU packaging standards
🔹 Prevents contamination & bacterial growth – Ensures hygienic storage
🔹 Tamper-evident seals – Provides consumer confidence in product integrity
📌 Supporting Sustainable Packaging Solutions
🔹 Recyclable material – Reduces plastic waste in food packaging
🔹 Lightweight & efficient – Decreases carbon footprint during transport
🔹 Compatible with biodegradable coatings – Allows eco-friendly customization
Using BOPP heat sealable film in food packaging aligns with global sustainability goals, ensuring minimal environmental impact while maintaining high packaging standards.
6. Choosing the Right BOPP Heat Sealable Film Supplier
To ensure optimal packaging performance, it is crucial to work with a trusted supplier. Key factors to consider include:
✔ Quality & Compliance – Certified for food safety & industry standards
✔ Customization Options – Available in various thicknesses & sizes
✔ High-Performance Features – Offers strong sealing, clarity, & printability
✔ Reliable Supply Chain – Ensures consistent production & fast delivery
Leading manufacturers like Chalvo Film offer premium BOPP heat sealable film, ensuring durability, efficiency, and sustainability in food packaging applications.
Contact us
At Chalvo, we understand the unique needs of businesses looking to enhance their packaging, marketing materials.
Our team is here to help you choose the right laminating films that not only meet your functional needs but also help elevate your brand’s visual appeal.