

EVOH Film
EVOH film provides an effective barrier against contaminants, ensuring the protection and quality of various products across different industries.
Commercial EVOH Film
The Optimal Solution for Your Food, Pharmaceutical, and Chemical Packaging Needs
Chalvo’s high-quality plastic packaging films ensure the integrity and safety of your products across various industries.
- High transparency and gloss
- Exllent Printing Capacity And Heat Sealing Strength
- Excellenet Separation From Oil And Acid
Excellent Evenness
Excllent Lamination Firmness.
Excellent Smoothness


Table Of Contents For This Page
To make sure you can find the information you want quickly,
we have prepared this content directory that will jump to the corresponding location when you click on it.






General Application For EVOH Film
EVOH Film has the following wide range of applications, Inquiry us for more solutions.
Food Package
Medical Packaging
Cosmetic Packaging
Electronic product packaging
Product Catalog
EVOH Film to Promote Your Business


Shrink Film
- Typical Thickness: 10 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>41.7MPa, TD>33.4MPa
- Feature: Uniform Shrinkage,
Clean Room Production,
Automated Quality Control, - Classic products:Heat Shrink Wrap Film, Pallet Shrink Wrap Film

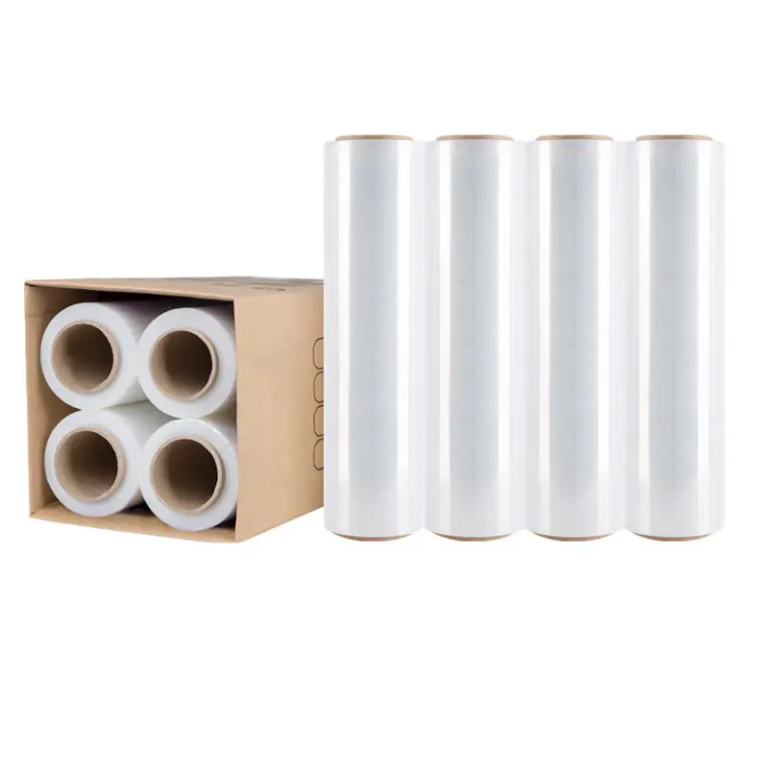
Winding Film
- Typical Thickness: 10 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>41.7MPa, TD>33.4MPa
- Feature: Superior Clarity,
Exceptional Strength,
Consistent Shrinkage - Classic products:

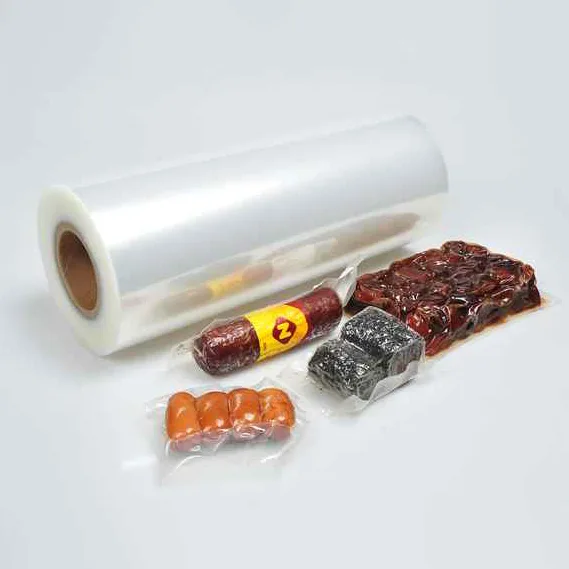
Vacuum Bag
- Typical Thickness: 45 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>35MPa, TD>25MPa
- Feature: Good smoothness, anti-static effect, good flatness, good plasticization,
- Classic products:
Clear Vacuum Bag
Matt Vacuum Bag


Functional Film
- Typical Thickness: 20-50 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>130MPa, TD>240MPa
- Feature: Good antistatic performance,
Excellent anti-fogging performance - Classic products:
What People Are Saying?
A Brief Self-Nomination, Why Choose Chalvo?

Reliable EVOH Films Manufacturer in China
- Larger Capacity, Better Price. Annual production up to 50,000 tons & lower wholesale price
- Lower MOQ, More Flexibility. Save you more and generate higher profitability with 500KG MOQ
- Certified Products, Safety Guaranteed.Compliance of ISO and EN, strictly production to guarantee quality.
Frequently Asked Questions
If the Films reach you and for whatever reason you are not satisfied you should notify CHALVO within 7 days of receiving the Films and we will replace or rework for free.
We generally request customers work to our standard payment terms for at least the first order. These are 50% deposit and 50% prior to shipping. It is possible to negotiate other payment terms such as Net 30, but these are agreed on a case by case basis.
Stage One: full DFM at time of quotation by highly experienced engineers. They will highlight any problem areas or make suggestions for changes. Stage Two: incoming inspection of materials with our own Gas Transmission Rate Tester Stage Three: Full QC inspection and report before shipping
We generally request customers work to our standard payment terms for at least the first order. These are 50% deposit and 50% prior to shipping. It is possible to negotiate other payment terms such as Net 30, but these are agreed on a case by case basis.
CHALVO is currently certified ISO22000 /BST/SGS
We aim to quote all prototype projects within 24 hours. All General packaging projects within 24 hours. All non-conventional packaging projects within 3 days. There are sometimes processes and materials which CHALVO does not offer in house; these could add time to the quotation and will be highlighted as and when.
All projects are DDU unless otherwise stated. This means the quote includes all freight and charges to a port of your choice. Any and all import and other taxes in your country are your own responsibility. If you require different shipping terms these can be negotiated on a case by case basis.
We accept payment via bank transfer to China.
More Related Flexible Packaging Film Supplies
The Smart Way To Improve Your Business

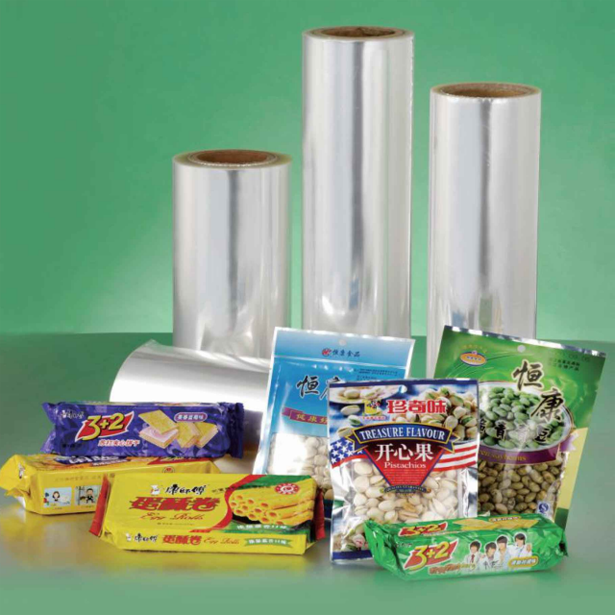
BOPP FILM
- High gloss and translucency for better display of products
- Excellent odor barrier to prevent fragrance leakage
- Good oxygen and water vapor barrier performance
- Excellent stretch forming uniformity, efficient water
- resistance to effectively maintain the locking of packaged meat products moisture
- Surface treatment is available for lamination
- Good resistance to wear and heat sealing properties


PET FILM
- High gloss
- Excellent gas isolation
- Excellent light-blocking properties
- Moisture resistant, high temperature resistant

BOPA FILM
- Uniform Shrinkage
- Clean Room Production
- Automated Quality Control
- High transparent
EVOH Film: The Ultimate Guide(2026)

EVOH film, which stands for ethylene-vinyl alcohol copolymer, is a popular material for food packaging. It’s good at keeping oil out, keeping oxygen out, and not getting staticky. In this article, we’re going to talk about how EVOH is made, the problems it has, and what’s happening with it right now. We’ll also talk about where EVOH is going in the future and what you need to look for when you’re picking a film supplier. Hope this article helps you out.
Table Of Contents
9. Classification and Applications of EVOH Film
9.1 Tissue Film
9.2 Retort Film
9.3 Inflatable Film
Development History of EVOH
EVOH (Ethylene-Vinyl Alcohol Copolymer) traces its origins back to the mid-20th century when researchers discovered its exceptional barrier properties. Initially, EVOH was developed to replace traditional PVDC resins, providing better packaging solutions. With continuous technological advancements, EVOH’s application range has expanded, making it an essential component in various packaging materials
The introduction of EVOH marked a significant milestone in the evolution of packaging materials. Researchers and engineers were able to develop a material that not only met the demanding requirements of food and beverage packaging but also addressed the environmental concerns associated with traditional packaging materials. As a result, EVOH has become a preferred choice for many manufacturers looking to enhance the quality and safety of their products.
What is EVOH Film?
EVOH is a copolymer of ethylene and vinyl alcohol. It is known for its excellent gas barrier properties, which protect products from oxygen and moisture, thereby extending shelf life. Its versatility allows it to be used in various forms, including films, bottles, and containers.
EVOH’s unique chemical structure gives it the ability to create an impermeable barrier against gases and organic solvents. This property is crucial in maintaining the freshness and quality of perishable goods, making EVOH an indispensable material in the food packaging industry. Additionally, its resistance to chemicals and environmental stressors makes it suitable for a wide range of applications beyond food packaging.
The Difference Between EVOH Film and PVDC Film
PVDC (polyvinylidene chloride) and EVOH (ethylene-vinyl alcohol copolymer) films are two common high barrier packaging materials, each with different properties and applications. Here are the detailed differences between them:
Chemical composition
PVDC: Made by polymerizing vinylidene chloride (VDC) and other comonomers,
EVOH: Made by copolymerizing ethylene and vinyl alcohol, its barrier properties depend on the content of vinyl alcohol.
Barrier properties
PVDC: It has extremely high barrier properties and has very good barrier effects on oxygen, moisture, and aroma. It is widely used in food packaging that needs to be stored for a long time.
EVOH: It mainly provides oxygen barrier, and has a general barrier effect on moisture. It is often used in combination with other materials to enhance moisture barrier properties.
Transparency
PVDC: It has relatively low transparency and usually appears slightly yellow or green.
EVOH: It has high transparency and is suitable for packaging applications that require high transparency, such as food and medical packaging.
Heat sealing performance
PVDC: It has good heat sealing performance and can achieve effective heat sealing at lower temperatures.
EVOH: It has poor heat sealing performance and needs to be used in combination with other materials with heat sealing performance.
Environmental performance
PVDC: Because it contains chlorine, harmful chlorides may be produced during incineration or degradation, which has a certain impact on the environment.
EVOH: It does not contain chlorine, does not produce harmful substances during incineration, and is relatively environmentally friendly.
Application areas
PVDC: It is mainly used for packaging with high barrier requirements, such as food packaging (meat, dairy products, frozen food, etc.), medical packaging, cosmetic packaging, etc.
EVOH: It is mainly used for packaging that requires high transparency and high oxygen barrier, such as food packaging (beverage bottles, meat packaging), medical device packaging, cosmetic packaging, etc.
Price
PVDC: Since PVDC film is usually a single-layer structure, the price is relatively low.
EVOH: The price is relatively high because EVOH film is usually a composite film and needs to be laminated with other materials (such as PE, PP, etc.) to form a film, so the overall cost will be higher than that of PVDC film.
Processing performance
PVDC: It usually adopts the film blowing process, so it is more complicated and has strict requirements on processing conditions, requiring specific processing equipment and technology.
EVOH: It is relatively easy to process and can be produced using conventional plastic processing equipment, but it is necessary to pay attention to its sensitivity to moisture.
In summary, PVDC and EVOH films each have their own advantages and disadvantages, and the specific selection should be comprehensively considered based on packaging requirements and application scenarios.PVDC and EVOH are specialized polymers for packaging, with PVDC providing superior barrier properties at a lower cost but with transparency and environmental drawbacks, while EVOH delivers high transparency and eco-friendliness at a higher price, needing lamination for improved performance. The choice hinges on the desired balance of cost, barrier effectiveness, environmental impact, and aesthetic requirements for the packaging application.
Why is EVOH Designed For?
EVOH film is designed for a variety of applications due to its beneficial properties, such as:
- Packaging:
Commonly used in food packaging, including snack foods, confectionery, fresh produce, and baked goods. Its clarity, strength, and barrier properties make it ideal for preserving and displaying products.
- Labels:
Used for labeling, especially in the beverage industry, where its durability and printability are essential.
- Lamination:
Often used in lamination with other materials to enhance their strength and protective qualities.
- Printing:
Widely used for various printed materials and advertising displays due to its excellent printability.
EVOH film’s versatility extends beyond traditional packaging applications. It is also used in the medical field for sterile packaging of medical devices and pharmaceuticals. The material’s ability to prevent contamination and maintain sterility makes it a valuable asset in healthcare settings. Moreover, EVOH is utilized in the construction industry for vapor barriers, contributing to the longevity and integrity of buildings.
Is EVOH Film Safe?
Yes, EVOH film is considered safe for use in food packaging. It complies with various food safety regulations and standards globally, ensuring that it does not react with food products or affect their quality.
EVOH has undergone rigorous testing to ensure its safety for direct contact with food. It meets the stringent requirements set by regulatory bodies such as the FDA (Food and Drug Administration) in the United States and the EFSA (European Food Safety Authority) in Europe. These certifications provide manufacturers and consumers with confidence in the material’s safety and reliability.
How to Choose the Right EVOH Film?
Choosing the right EVOH film depends on your specific needs. Consider factors such as the type of product being packaged, required barrier properties, clarity, and strength. Working with a knowledgeable supplier can help you select the optimal film for your application.
When selecting EVOH film, it is essential to assess the specific requirements of your application. For instance, high-barrier EVOH films are ideal for products that require extended shelf life, such as vacuum-sealed meats and dairy products. On the other hand, low-barrier EVOH films may be more suitable for products with shorter shelf lives or those that require less stringent protection. Collaborating with a supplier who understands these nuances can significantly enhance the performance and efficiency of your packaging solutions.
How is EVOH Film Produced
The production of EVOH film involves several key steps:
Raw Materials Preparation
Ethylene and Vinyl Alcohol Acquisition: The main raw materials for EVOH are ethylene and vinyl alcohol, obtained through chemical synthesis.
Polymerization Process
Polymerization Steps and Conditions: Ethylene and vinyl alcohol undergo polymerization under specific conditions to form EVOH copolymer.
Extrusion
The extrusion process is critical in determining the final properties of the EVOH film. Parameters such as temperature, pressure, and extrusion speed must be meticulously controlled to ensure the film’s uniformity and performance. Advanced extrusion technologies have enabled the production of EVOH films with enhanced barrier properties and mechanical strength.The EVOH resin is melted and extruded through a flat die to form a thin film.Extrusion
Cooling
The extruded film is rapidly cooled to solidify its structure.
Rapid cooling is essential to lock in the desired properties of the EVOH film. This step prevents the formation of defects and ensures that the film maintains its clarity and barrier effectiveness. Cooling methods, such as air or water quenching, are employed to achieve the optimal film characteristics.
Biaxial Stretching
The film undergoes biaxial stretching, where it is stretched both longitudinally and transversely to enhance its strength and barrier properties.
Biaxial stretching aligns the polymer chains in the EVOH film, significantly improving its tensile strength and gas barrier performance. This step is crucial for applications that demand high mechanical stability and durability, such as vacuum packaging and industrial laminates.
Further Cooling
After stretching, the film is further cooled and wound onto rolls for subsequent processing or shipment.
The final cooling step stabilizes the stretched film, ensuring that it retains its enhanced properties during storage and transportation. The EVOH film is then inspected for quality assurance before being wound onto rolls and prepared for delivery to customers.
EVOH Film Properties for Packaging
EVOH film is an efficient, transparent, antistatic, and weather-resistant material that provides excellent oxygen barrier properties, ensuring the freshness and longevity of packaged foods while supporting high-definition printing.
Physical properties
High processing efficiency
It allows for thickness reduction. It results in a more economical structure and reduces environmental impact.
- Excellent transparency
EVOH has excellent oxygen barrier properties to protect valuable food ingredients. It also ensures packaging contents remain fresh throughout the supply chain. It includes a guarantee during long-term storage. It also reduces and eliminates the need for added preservatives. Additionally, it enables longer shelf life of food packaged in an improved atmosphere without loss of quality.
- Antistatic properties
EVOH is a strong antistatic polymer. When used as a surface layer, it prevents dust from adhering to packaging. It can be very beneficial to use, especially if you are in the food industry.
- Weather resistance
EVOH plastic food packaging is very resistant to the effects of natural factors. The polymer does not change color even when exposed to sunlight; it neither becomes opaque nor yellows. Changes in mechanical mass were negligible, indicating good resilience to the overall impact of weather.
Chemical properties
- Excellent oxygen barrier properties
EVOH has excellent oxygen barrier properties and can protect valuable food ingredients. It also ensures packaging contents remain fresh throughout the supply chain. It includes a guarantee during long-term storage. It also reduces and eliminates the need for added preservatives. Additionally, it enables longer shelf life of food packaged in an improved atmosphere without loss of quality.
- Resistant to organic solvents
EVOH plastic food packaging is very resistant to the effects of natural factors. The polymer does not change color even when exposed to sunlight; it neither becomes opaque nor yellows. Changes in mechanical mass were negligible, indicating good resilience to the overall impact of weather.
Other properties
Support high-definition printing
Classification and Applications of EVOH Film
EVOH (Ethylene Vinyl Alcohol) film is a specialized packaging material known for its excellent gas barrier properties, which makes it ideal for applications requiring extended shelf life and protection against oxygen, moisture, and other gases. Here’s a detailed look at the classification and applications of EVOH film:
Classification of EVOH Film
EVOH films are typically classified based on their specific composition, thickness, and intended use:
High-Barrier EVOH Film:
- Characteristics: These films have a high content of vinyl alcohol units, which provide exceptional gas barrier properties, especially against oxygen and carbon dioxide. They are used where the highest level of protection is required.
- Applications: Used in packaging applications where the prevention of oxidation is critical, such as for meat, fish, dairy products, and pharmaceuticals.
Medium-Barrier EVOH Film:
- Characteristics: With a balanced composition of ethylene and vinyl alcohol units, these films offer a moderate level of gas barrier, combined with good flexibility and ease of processing.
- Applications: Ideal for packaging products that require good but not extreme barrier properties, such as snacks, processed foods, and certain medical supplies.
High-Ethylene EVOH Film:
- Characteristics: These films have a higher ethylene content, which enhances their moisture resistance and flexibility but reduces their gas barrier effectiveness. They are more suitable for packaging applications where moisture barrier and flexibility are more critical than gas barrier.
- Applications: Used for products like fresh produce packaging, where flexibility and moisture resistance are needed, but the gas barrier is less of a concern.
Laminated or Co-extruded EVOH Film:
- Characteristics: These films are laminated or co-extruded with other materials such as polyethylene (PE), polypropylene (PP), or polyethylene terephthalate (PET) to enhance mechanical properties and sealability, while retaining the gas barrier properties of EVOH.
- Applications: Commonly used in multi-layer packaging structures to combine the benefits of various materials, making them suitable for a wide range of food and non-food packaging applications.
Applications of EVOH Film
EVOH film is used in various industries due to its unique combination of barrier properties and versatility:
Food Packaging:
- Processed Foods: EVOH films are widely used for packaging processed foods like meats, sausages, ready-to-eat meals, and dairy products that are susceptible to oxidation. The film’s high barrier properties protect the flavor, color, and nutritional value of the food by preventing oxygen ingress.
- Beverage Packaging: EVOH films are used in multi-layer beverage containers and pouches for juices, dairy drinks, and other liquid products to extend shelf life by protecting against oxygen and carbon dioxide.
- Snack Packaging: Used for packaging snacks, nuts, and dried fruits where extended shelf life and protection against oxidation and moisture are needed.
Pharmaceutical and Medical Packaging:
- Pharmaceutical Blister Packs: EVOH films provide a high barrier against oxygen and moisture, making them ideal for packaging tablets, capsules, and other pharmaceuticals that are sensitive to environmental factors.
- Medical Device Packaging: Used for packaging medical devices and supplies that require protection from oxygen and moisture, such as syringes, catheters, and diagnostic equipment.
Cosmetics and Personal Care Packaging:
- Skincare and Haircare Products: EVOH films are used in the packaging of lotions, creams, shampoos, and other personal care products to prevent oxidation and maintain product efficacy and freshness.
- Perfume and Fragrance Packaging: Provides an effective barrier against oxygen and volatile compounds, preserving the fragrance and extending the shelf life of perfumes.
Industrial Packaging:
- Chemical Packaging: EVOH films are used for packaging chemicals, adhesives, and solvents that are sensitive to oxygen or require a controlled environment to maintain stability and efficacy.
- Agricultural Chemicals: Used for packaging agricultural chemicals, such as pesticides and herbicides, to prevent degradation from exposure to air and moisture.
Automotive Applications:
- Fuel System Components: In the automotive industry, EVOH films are used in fuel tanks and fuel lines to prevent the permeation of gasoline vapors, helping to reduce emissions and comply with environmental regulations.
Flexible Packaging Solutions:
- Pouches and Bags: EVOH films are often used in flexible packaging solutions, such as vacuum bags, stand-up pouches, and retort pouches, where their high barrier properties help extend the shelf life of food and non-food items.
- Laminates and Co-extrusions: As part of multi-layer structures, EVOH films contribute to the overall barrier performance of flexible packaging, enhancing the durability and protective qualities of the packaging.
EVOH films are essential in applications that demand high barrier properties against gases, odors, and moisture. Their versatility and effectiveness make them a valuable material in various packaging and industrial applications.


Challenges Faced by EVOH Film
EVOH film manufacturers face the dual challenge of meeting stringent environmental regulations and intense market competition while innovating and managing fluctuating raw material costs.
Environmental Pressures and Regulatory Compliance
EVOH films must meet stringent environmental regulations and standards. Balancing performance with eco-friendliness is a significant challenge for manufacturers.
The increasing demand for sustainable packaging solutions has prompted manufacturers to explore eco-friendly alternatives to traditional EVOH films. While EVOH offers excellent barrier properties, its production and disposal pose environmental challenges. Manufacturers are investing in research and development to create biodegradable or recyclable EVOH films that meet regulatory requirements and consumer expectations for sustainability.
Market Competition
The packaging industry is highly competitive, with constant pressure to innovate and improve. EVOH films face competition from other high-barrier materials and emerging technologies.
The competitive landscape of the packaging industry drives continuous innovation and improvement. EVOH films must compete with other high-barrier materials, such as polyethylene terephthalate (PET) and polyvinylidene chloride (PVDC). Additionally, emerging technologies, such as nanocomposites and bio-based polymers, pose potential challenges to the market dominance of EVOH. To stay ahead, manufacturers must invest in research and development to enhance the performance and sustainability of EVOH films.
Material Innovation and Raw Material Cost Fluctuations
EVOH film producers face a challenge and an opportunity when it comes to making new stuff. On one hand, people always want new and better materials that do more, cost less, and don’t mess up the environment. On the other hand, making new stuff takes a lot of time and money.
Another thing that makes things hard is the cost of the stuff you need to make EVOH films. The cost of ethylene and vinyl alcohol, the main ingredients in EVOH, can change based on what’s going on in the world, the price of oil, and how things are going in the supply chain. These changes can mess up how much it costs to make EVOH films and how much you can charge for them. You have to be good at dealing with these changes to make money and sell stuff.
Making new blends or composites that make EVOH better or easier to recycle is important for keeping it useful in packaging. The challenge is finding a way to make new stuff that doesn’t cost too much.
Noted: From the establishment of Chalvo to the present, it has deeply involved in plastic flexible film for more than 10 years and has always been committed to improving the process. In 2012, completed a 5-layer EVOH film in the Sichuan factory, and in 2014, extruded a 9-layer configuration in the Zhejiang factory.
How to Choose the Right EVOH Film Supplier
When selecting a EVOH film supplier, several key factors must be considered to ensure you get the best value and service.
Expertise
Evaluate the supplier’s expertise in EVOH packaging industry. Experienced suppliers are more likely to provide high-quality products and innovative solutions.
Pricing
Competitive pricing is essential for maintaining profitability. Compare prices from different suppliers to make sure you get the best deal without sacrificing quality.
Delivery
Timely delivery is important to keep your production schedule on track. Ensure the supplier has a reliable delivery system in place.
Customer Service & Reviews
Good customer service can make a big difference in your overall experience. Check reviews and testimonials from other clients to gauge the supplier’s reliability and customer service quality.
EVOH Film and CHALVO
CHALVO is a company that specialises in customised packaging solutions as well as production. Feel free to send us any content on packaging, progress and growth together will be our constant theme.
REQUEST A QUOTE
We will contact you within 1 working day, please pay attention to the email with the suffix “@chalvo.com”.