

BOPE Film
BOPE film provides an effective barrier against contaminants, ensuring the protection and quality of various products across different industries.
Commercial BOPE Film
The Optimal Solution for Your Food, Pharmaceutical, and Chemical Packaging Needs
Chalvo’s high-quality plastic packaging films ensure the integrity and safety of your products across various industries.
- High transparency and gloss
- Exllent Printing Capacity And Heat Sealing Strength
- Excellenet Separation From Oil And Acid
Excellent Evenness
Excllent Lamination Firmness.
Excellent Smoothness


Table Of Contents For This Page
To make sure you can find the information you want quickly,
we have prepared this content directory that will jump to the corresponding location when you click on it.





General Application For BOPE Film
BOPE Film has the following wide range of applications, Inquiry us for more solutions.
Food Package
Pallet Wrapping
Industrial Packaging
Heat shrink packaging
Product Catalog
BOPE Film to Promote Your Business
Shrink Film
- Typical Thickness: 10 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>41.7MPa, TD>33.4MPa
- Feature: Uniform Shrinkage,
Clean Room Production,
Automated Quality Control, - Classic products:Heat Shrink Wrap Film, Pallet Shrink Wrap Film

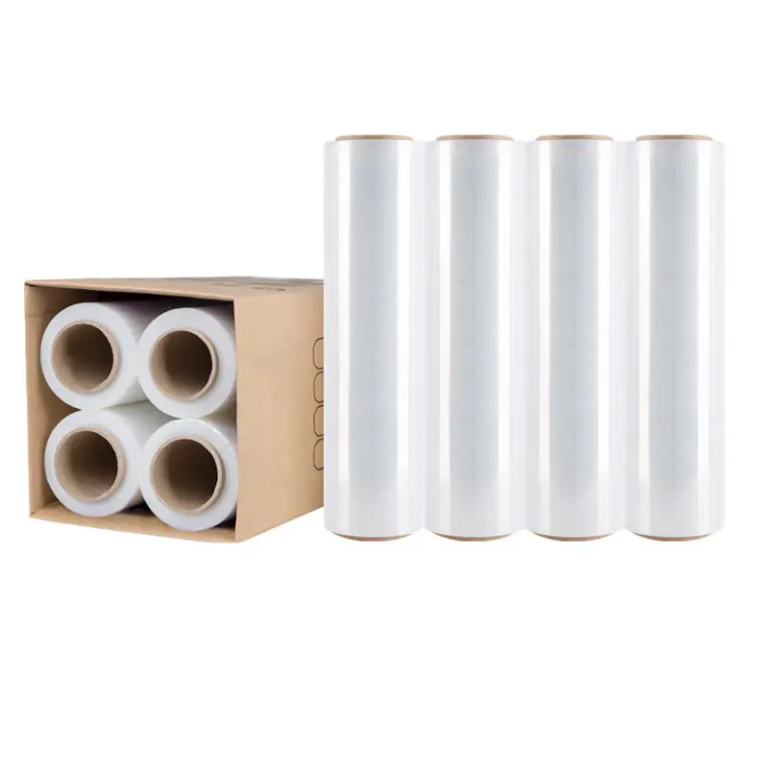
Winding Film
- Typical Thickness: 10 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>41.7MPa, TD>33.4MPa
- Feature: Superior Clarity,
Exceptional Strength,
Consistent Shrinkage - Classic products:

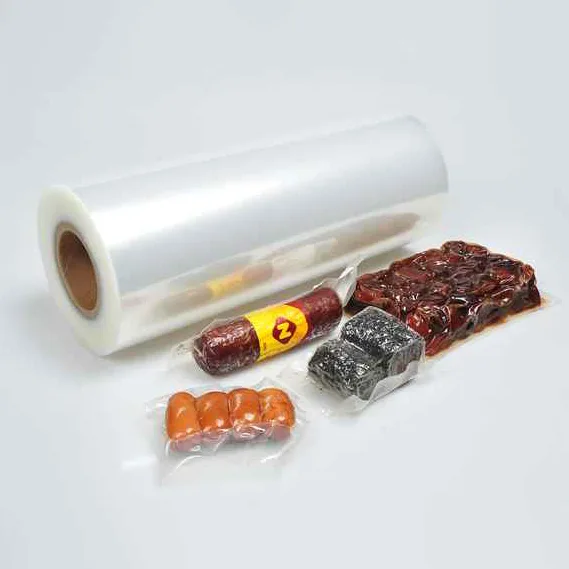
Vacuum Bag
- Typical Thickness: 45 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>35MPa, TD>25MPa
- Feature: Good smoothness, anti-static effect, good flatness, good plasticization,
- Classic products:
Clear Vacuum Bag
Matt Vacuum Bag


Functional Film
- Typical Thickness: 20-50 mic, Spercial specifications can be customized according to customer requirements.
- Tensile Srength: MD>130MPa, TD>240MPa
- Feature: Good antistatic performance,
Excellent anti-fogging performance - Classic products:
A Brief Self-Nomination, Why Choose Chalvo?

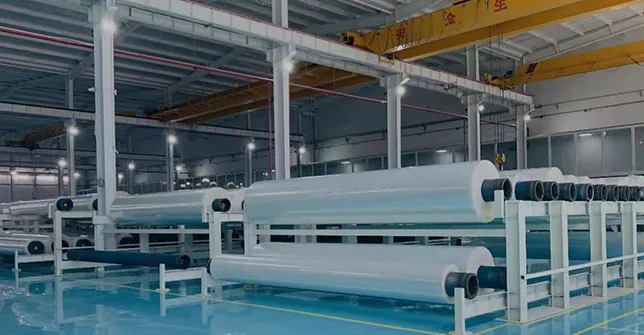
Reliable BOPE Films Manufacturer in China
- Larger Capacity, Better Price. Annual production up to 50,000 tons & lower wholesale price
- Lower MOQ, More Flexibility. Save you more and generate higher profitability with 500KG MOQ
- Certified Products, Safety Guaranteed.Compliance of ISO and EN, strictly production to guarantee quality.
Frequently Asked Questions
If the Films reach you and for whatever reason you are not satisfied you should notify CHALVO within 7 days of receiving the Films and we will replace or rework for free.
We generally request customers work to our standard payment terms for at least the first order. These are 50% deposit and 50% prior to shipping. It is possible to negotiate other payment terms such as Net 30, but these are agreed on a case by case basis.
Stage One: full DFM at time of quotation by highly experienced engineers. They will highlight any problem areas or make suggestions for changes. Stage Two: incoming inspection of materials with our own Gas Transmission Rate Tester Stage Three: Full QC inspection and report before shipping
We generally request customers work to our standard payment terms for at least the first order. These are 50% deposit and 50% prior to shipping. It is possible to negotiate other payment terms such as Net 30, but these are agreed on a case by case basis.
CHALVO is currently certified ISO22000 /BST/SGS
We aim to quote all prototype projects within 24 hours. All General packaging projects within 24 hours. All non-conventional packaging projects within 3 days. There are sometimes processes and materials which CHALVO does not offer in house; these could add time to the quotation and will be highlighted as and when.
All projects are DDU unless otherwise stated. This means the quote includes all freight and charges to a port of your choice. Any and all import and other taxes in your country are your own responsibility. If you require different shipping terms these can be negotiated on a case by case basis.
We accept payment via bank transfer to China.
More Related Flexible Packaging Film Supplies
The Smart Way To Improve Your Business


EVOH FILM
- High gloss and translucency for better display of products
- Excellent odor barrier to prevent fragrance leakage
- Good oxygen and water vapor barrier performance
- Excellent stretch forming uniformity, efficient water
- resistance to effectively maintain the locking of packaged meat products moisture
- Surface treatment is available for lamination
- Good resistance to wear and heat sealing properties


PET FILM
- High gloss
- Excellent gas isolation
- Excellent light-blocking properties
- Moisture resistant, high temperature resistant

BOPA FILM
- Uniform Shrinkage
- Clean Room Production
- Automated Quality Control
- High transparent
BOPE Film: The Ultimate Guide(2026)

BOPE film, or Biaxially Oriented Polyethylene film, is a cutting-edge material in the packaging industry, known for its excellent strength, clarity, and recyclability. As businesses and manufacturers seek sustainable packaging solutions, BOPE film emerges as a superior choice due to its unique properties and versatility. This guide provides a comprehensive overview of BOPE film, detailing its development, properties, and diverse applications, and highlighting why it is becoming an essential material in various industries. From understanding the benefits and safety of BOPE films to learning how to choose the right type and supplier, this article equips you with all the necessary information to make informed decisions about BOPE film.
Table Of Contents
3. The Difference Between BOPE Film and Other Films
3.1 BOPE VS BOPP
3.2 BOPE VS PET
3.3 BOPE VS CPP
9. Classification and Applications of BOPE Film
9.1 Tissue Film
9.2 Retort Film
9.3 Inflatable Film
Development History of POPE
The development of BOPE film began as industries searched for materials that could provide both superior performance and sustainability. With advancements in polymer technology and manufacturing processes, BOPE films were developed to meet these needs, offering high strength, transparency, and recyclability. Over the years, BOPE films have evolved, incorporating new formulations and processes to improve their properties and expand their use in packaging.
What is BOPE Film?
BOPE film, short for Biaxially Oriented Polyethylene Film, is made from polyethylene resin with a unique molecular structure. It undergoes biaxial orientation, a process that stretches the film in two directions, enhancing its mechanical properties such as tensile strength and impact resistance, making it ideal for various packaging applications.
The Difference Between BOPE Film and Other Films
BOPE films are often compared with other types of films, such as BOPP, PET, and CPP. Understanding the differences between these films can help you choose the right material for your packaging needs.
BOPE VS BOPP
While both BOPE (Biaxially Oriented Polyethylene) and BOPP (Biaxially Oriented Polypropylene) films are used for packaging, there are some key differences:
- Material Composition: BOPE is made from polyethylene, whereas BOPP is made from polypropylene.
- Properties: BOPE films are softer and more flexible compared to the stiffer BOPP films. BOPP provides better moisture vapor barriers, while BOPE offers better impact resistance and sealability.
- Applications: BOPP is often used for snack food packaging due to its moisture barrier, whereas BOPE is preferred for applications requiring toughness and clarity.
- BOPE VS PET
BOPE and PET (Polyethylene Terephthalate) films differ primarily in their material properties:
- Heat Resistance: PET films offer superior heat resistance, making them suitable for high-temperature applications. BOPE films, while offering good heat sealing properties, are not as heat resistant as PET.
- Recyclability: BOPE is easier to recycle due to its polyethylene base, aligning with the growing demand for sustainable packaging solutions.
- Barrier Properties: PET provides a stronger barrier against gases and odors, while BOPE offers flexibility and durability.
- BOPE VS CPP
CPP (Cast Polypropylene) and BOPE films are both used in packaging but serve different purposes:
- Manufacturing Process: CPP is produced through a casting process, whereas BOPE is produced through a biaxial orientation process.
- Properties: BOPE films have superior mechanical strength and clarity, while CPP films offer better puncture resistance and are softer to the touch.
- Applications: BOPE is ideal for applications requiring high strength and clarity, such as retail bags, while CPP is often used for packaging where high clarity and flexibility are needed.
While CPP, BOPP, PET, and BOPE films all serve as essential materials in the packaging industry, each has unique characteristics that make it suitable for specific applications. CPP film is valued for its flexibility and heat sealing properties, making it ideal for food packaging and retort bags. BOPP film, with its excellent strength and transparency, is preferred for printing and display packaging. PET film stands out with its high strength and chemical resistance, suitable for high-demand packaging like food, beverages, and electronics. PE film, known for its waterproof and chemical-resistant properties, is widely used in various packaging applications, from plastic bags to agricultural films. Understanding these differences enables more informed decisions when selecting the appropriate material for specific packaging needs.
Why is BOPE Designed For?
BOPE films are designed to provide high performance in packaging applications. They are engineered to be strong, durable, and flexible, making them suitable for a wide range of products, including food packaging, consumer goods, and industrial materials. The material’s ability to combine strength with clarity and its recyclability make it an attractive option for companies looking to enhance their packaging solutions while reducing environmental impact.
Is BOPE Film Safe?
Yes,BOPE film is considered safe for use in various packaging applications, including food contact materials. The polyethylene resin used in BOPE films is approved by regulatory bodies such as the FDA and EU for direct food contact, ensuring it does not pose a risk to consumers. Additionally, the manufacturing processes for BOPE films are designed to minimize contaminants, making them a reliable choice for safe packaging.
How to Choose the Right BOPE Film?
Choosing the right BOPE film for your packaging needs involves considering several factors:
- Thickness and Durability
The thickness of the CPP film is an important factor to consider, as it determines the film’s durability and strength. Thicker films offer better protection against punctures and tears, making them ideal for packaging heavy or sharp-edged products.
- Clarity and Gloss
Clarity and gloss are critical properties for packaging applications where product visibility is important. BOPE films with high clarity and gloss enhance the visual appeal of the packaged product, making it more attractive to consumers.
- Heat-Sealing Strength
The heat-sealing strength of BOPE films is another key consideration. Films with higher heat-sealing strength create more secure seals, reducing the risk of package failure during transportation and storage.
- Barrier Properties
While BOPE films offer good moisture and chemical resistance, they may need to be combined with other materials if high barrier properties are required. For example, when packaging products that require protection from oxygen or light, BOPE films can be laminated with materials that provide additional barrier protection.
- Compatibility with Packaging Equipment
It is essential to choose a BOPE film that is compatible with your existing packaging equipment. Different films have different sealing requirements, and selecting the wrong film can lead to inefficiencies in your packaging process.
- Supplier Reliability
Finally, the reliability of your BOPE film supplier is a critical factor. A reliable supplier will not only provide consistent quality but will also offer technical support and flexible delivery options to meet your specific needs.
How is BOPE Film Produced
BOPE film production involves several steps:
- Extrusion: Polyethylene resin is melted and extruded through a flat die to form a continuous sheet of film.
- Biaxial Orientation: The film is stretched in both the machine direction (MD) and transverse direction (TD), enhancing its mechanical properties.
- Heat Setting: The film is heated and cooled under tension to stabilize its dimensions and improve clarity and gloss.
- Slitting and Winding: The finished film is slit to the desired width and wound onto rolls for further processing or packaging.
BOPE Film Properties for Packaging
BOPE films offer several properties that make them ideal for packaging applications:
- Durability: High tensile and impact strength ensure packaging remains intact during handling and transport.
- Barrier Properties: While not as strong as PET, BOPE provides a reasonable barrier against moisture and gases, suitable for various packaging needs.
- Versatility: BOPE films can be used in a wide range of packaging formats, including pouches, bags, and wraps.
- Environmental Benefits: BOPE films are fully recyclable, making them an environmentally friendly option for sustainable packaging solutions.
Classification and Applications of CPP Film
There are lots of different kinds of BOPE film. People make different kinds of BOPE film for different things. Based on the film that people make now, there are a few different kinds of BOPE film: Shrink Film, Winding Film, Vacuum Bag and Functional Film.
1. Shrink Film
- Description: BOPE shrink films are designed to shrink tightly around objects when heat is applied, creating a secure and protective covering. These films are made from biaxially oriented polyethylene and exhibit excellent clarity and gloss, allowing the packaged product to be visible while providing a tight seal.
- Common Applications:
- Consumer Goods Packaging: Used for packaging products such as CDs, DVDs, software boxes, and promotional packages, where product visibility and tamper evidence are important.
- Food Packaging: Employed in packaging perishable goods like fruits, vegetables, and baked goods, providing a clear, moisture-resistant barrier that extends shelf life.
- Bundling and Multipackaging: Ideal for bundling multiple items together, such as beverage cans or bottles, creating a compact, easy-to-handle package.
2. Winding Film
- Description: Winding films, also known as stretch films, are BOPE films designed to be stretched over products to hold them tightly together during transportation and storage. These films are highly elastic and provide excellent tensile strength, making them ideal for securing loads on pallets.
- Common Applications:
- Pallet Wrapping: Used extensively in logistics and warehousing to secure goods on pallets, preventing movement and damage during transit.
- Industrial Packaging: Protects products from dust, dirt, and moisture while being stored or shipped. Often used for irregularly shaped or heavy items that need a secure wrap.
- Protective Covering: Provides a protective layer over items like furniture or electronics during storage or transport, shielding them from scratches, dust, and environmental factors.
3. Vacuum Bag
- Description: BOPE vacuum bags are specialized films designed for vacuum packaging, which involves removing air from the package before sealing. This type of film has high barrier properties that prevent the ingress of oxygen, moisture, and contaminants, ensuring extended freshness and shelf life.
- Common Applications:
- Food Packaging: Used for vacuum-packing meats, cheeses, seafood, and other perishable items to preserve freshness, flavor, and nutritional value by reducing oxidation and microbial growth.
- Medical and Pharmaceutical Packaging: Provides a sterile barrier for medical devices and pharmaceuticals, ensuring they remain uncontaminated and safe for use.
- Electronics and Industrial Components: Protects sensitive electronics and precision components from moisture, dust, and other environmental factors during storage and shipment.
4. Functional Film
- Description: Functional films are a versatile category of BOPE films designed for specific applications that require additional properties, such as UV resistance, anti-static capabilities, or enhanced barrier performance. These films are engineered to meet the unique requirements of specialized packaging applications.
- Common Applications:
- Agricultural Packaging: Provides UV protection for agricultural products such as seeds, pesticides, and fertilizers, ensuring product integrity in various environmental conditions.
- Electronics Packaging: Anti-static films protect electronic components and devices from static discharge during storage and transport, reducing the risk of damage.
- Pharmaceutical Packaging: Offers high barrier properties to protect sensitive drugs and chemicals from moisture, oxygen, and light, maintaining their efficacy and safety.


Challenges Faced by BOPE Film
While BOPE films offer numerous advantages, they also face several challenges:
Environmental Pressures and Regulatory Compliance
As with all plastic materials, BOPE films are subject to increasing environmental scrutiny. Manufacturers are under pressure to reduce the environmental impact of their products, which includes improving the recyclability of BOPE films and reducing the use of non-renewable resources in their production.
Market Competition
The packaging industry is highly competitive, with numerous materials vying for market share. BOPE films must compete with other films, such as BOPP, PET, and CPP, each of which has its own strengths and weaknesses. To remain competitive, BOPE film manufacturers must continually innovate and improve their products.
Material Innovation and Raw Material Cost Fluctuations
The cost of raw materials used in the production of BOPE films can fluctuate, affecting the price and availability of the final product. Manufacturers must stay ahead of these changes by optimizing their production processes and exploring new materials and additives that can enhance the performance of BOPE films while keeping costs under control.
Recycling and Sustainability
One of the biggest challenges for BOPE films is improving their sustainability. While BOPE films are recyclable, the recycling process can be complex and not widely available in all regions. Manufacturers are exploring ways to make BOPE films easier to recycle and to increase the use of recycled materials in their production.
How to Choose the Right BOPE Film Supplier
Choosing the right BOPE film supplier is crucial for ensuring the success of your packaging solutions. Here are some key factors to consider:
Expertise and Experience
Look for a supplier with extensive experience in the production of BOPE films. An experienced supplier will have a deep understanding of the material and its applications, allowing them to provide valuable insights and recommendations for your specific needs.
Quality and Certifications
Quality is paramount when selecting a BOPE film supplier. Ensure that the supplier adheres to international standards, such as ISO and EN, and that their products are certified for safety and performance. This will give you confidence that the BOPE films you receive meet the highest quality standards.
Competitive Pricing
While price is an important consideration, it should not be the sole factor in your decision. Look for a supplier who offers competitive pricing without compromising on quality. Consider the total value, including factors such as technical support, delivery reliability, and after-sales service.
Delivery and Logistics
Reliable delivery schedules are critical for maintaining your production timelines. Choose a supplier with a strong logistics network and a proven track record of on-time delivery. This will help you avoid delays and ensure that your packaging operations run smoothly.
Customer Service and Reviews
Customer service is a key indicator of a supplier’s reliability. Choose a supplier who is responsive to your inquiries and willing to provide technical support when needed. Additionally, check online reviews and testimonials to gauge the experiences of other customers with the supplier.
Flexibility and Customization
Your packaging needs may vary, so it’s important to choose a supplier who can offer flexibility and customization. Whether you need a specific film thickness, color, or surface treatment, a supplier who can accommodate your requirements will be a valuable partner.
Contact Information
Ensure that your supplier has accessible and responsive customer support. This is important for addressing any issues that may arise during your partnership. Having direct contact with your supplier can help resolve problems quickly and maintain a smooth working relationship.
BOPE Film and CHALVO
Understanding BOPE films and selecting the right supplier can significantly impact your product’s performance and cost efficiency. By staying informed about the latest developments and choosing a reliable supplier, you can leverage BOPE films to achieve better results in your packaging solutions. With the growing demand for flexible packaging and the continued innovation in BOPE film technology, now is the perfect time to explore the benefits of BOPE films for your packaging needs.
REQUEST A QUOTE
We will contact you within 1 working day, please pay attention to the email with the suffix “@chalvo.com”.